1. Global B2B Sourcing Overview: The Strategic Imperative of Running Outerwear
The global performance activewear market is experiencing an unprecedented shift. Outerwear, specifically high-performance running jackets, has evolved from seasonal accessories to core revenue drivers for endurance brands, marathon organizers, corporate wellness distributors, and athletic retail chains. When purchasing bulk running jackets wholesale, global buyers face a complex matrix of choices involving technical fabric weight (GSM), hydrostatic water resistance, moisture vapor transmission rates (MVTR), seam sealing, and tariff-optimized supply chain logistics.
According to recent industry data, the demand for lightweight, packable, windproof running outerwear has grown at a CAGR of over 7.4%. Modern endurance runners demand gear that seamlessly bridges extreme weather protection with micro-climate heat dissipation. For brand managers and B2B buyers, sourcing directly from an established OEM/ODM manufacturer like Alanic eliminates intermediaries, guarantees strict color matching across production lots, and dramatically reduces total landed costs.
B2B Executive Takeaway
Procuring bulk running jackets requires balancing thermal control, weight, and weather barrier properties. Working directly with Alanic unlocks bespoke custom design services without design fees, low factory-direct minimum order quantities (MOQs), and full private label tag customization.
2. Technical Product Categories & Sourcing Recommendations
To maximize sell-through and satisfy diverse climate requirements, buyers should diversify their running outerwear orders across four foundational technical tiers. Each tier addresses distinct weather conditions, athlete performance metrics, and target retail price points.
Featherweight Packable Windbreakers
Constructed from ultra-thin 70 GSM ripstop nylon or polyester. Wind-resistant up to 40 MPH with DWR (Durable Water Repellent) surface coating. Packs into its own chest pocket.
Waterproof Storm-Shell Running Jackets
Engineered with a 2.5-layer hydrophobic membrane. Features a 10,000mm hydrostatic head rating and 10,000g/m²/24h breathability index with fully taped seams.
Thermal Fleece-Lined Softshell Jackets
Designed for sub-zero training runs. Features 240 GSM brushed grid-fleece interior, wind-blocking front panels, and 4-way stretch back ventilation zones for maximum mobility.
360° Reflective Night-Running Shells
High-visibility fluorescent bases with heat-transferred 3M™ Scotchlite™ reflective glass-bead taping across key motion points (cuffs, shoulders, lower spine).
Technical Fabric & Manufacturing Specification Matrix
When evaluating suppliers for bulk running jackets wholesale, technical compliance determines garment durability and functional athletic performance. The matrix below details Alanic's standard manufacturing benchmarks for custom production:
| Garment Category | Primary Fabric Composition | GSM Weight | Water Resistance / Breathability | Recommended Printing / Branding Method |
|---|---|---|---|---|
| Ultra-Light Windbreaker | 100% Micro Ripstop Polyester / Nylon | 65 – 85 GSM | DWR Treated / High Windproof (CFM < 5) | Sublimation Printing / Screen Print / Heat Transfer |
| Marathon Race Shell | Poly-Spandex Blend + PU Membrane | 110 – 140 GSM | 10,000mm Hydrostatic / 10,000 MVTR | Seamless Bonding / Reflective Heat Seal Logo |
| Winter Hybrid Softshell | 3-Layer Composite Fleece + Wind Membrane | 220 – 280 GSM | Showerproof / High Thermal Retention | 3D Direct Embroidery / Woven Patch / Sublimation |
| Trail Running Anorak | Cordura® Reinforced Ripstop + Stretch Mesh | 130 – 160 GSM | PFC-Free Eco DWR / Laser Cut Venting | Sublimation / High-Density Rubber Print |
3. Product & Technology Trends: Outerwear Innovations (2026–2030)
The technical outerwear landscape is undergoing rapid innovation driven by advancements in textile chemistry, sustainable raw materials, and wearable ergonomics. Procurement managers must stay ahead of consumer expectations by integrating these key technological trends into their product lineups:
A. Sustainable Bio-Based & Recycled Synthetics
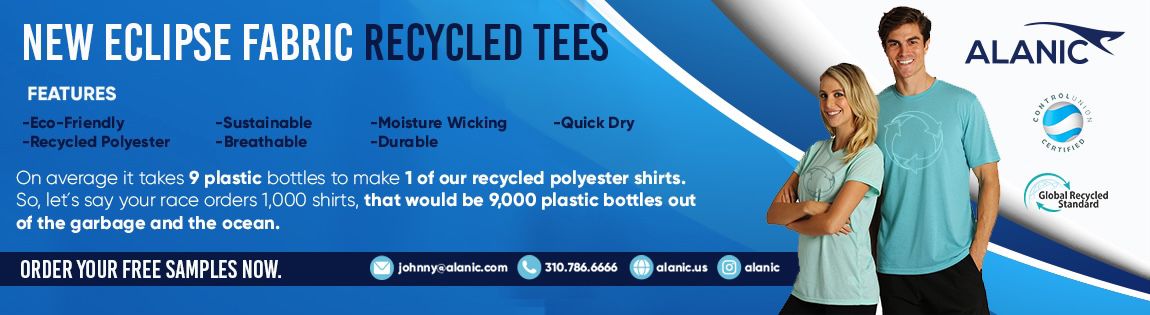
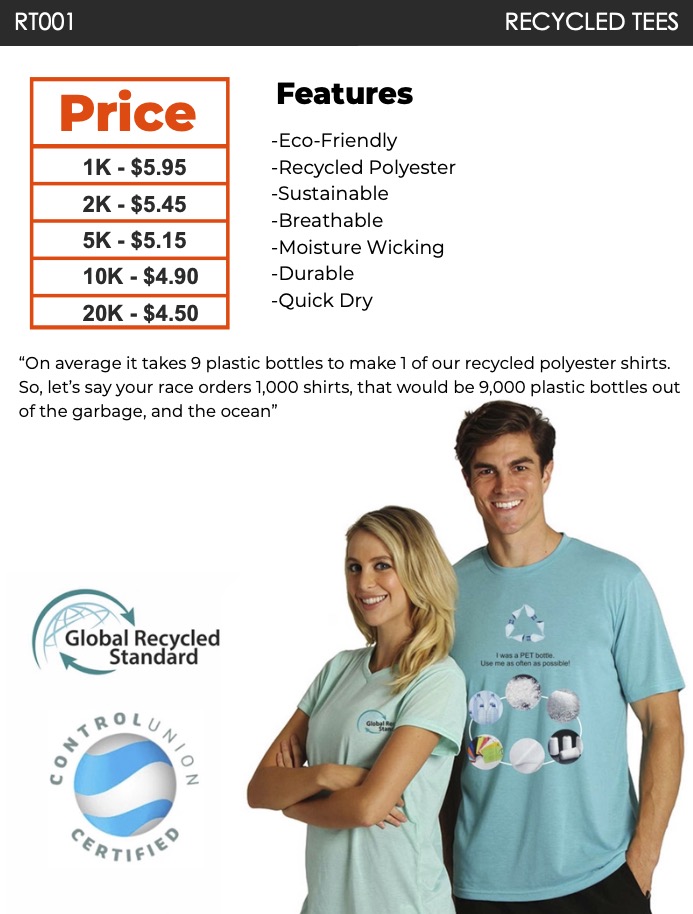
Modern consumers actively boycott petroleum-heavy virgin synthetics. Premium wholesale orders are transitioning toward Global Recycled Standard (GRS) certified recycled polyester (rPET) derived from post-industrial waste and ocean-bound plastics. Furthermore, bio-derived nylon membranes formulated from castor bean oil are setting new benchmarks for eco-friendly waterproof performance, matching traditional PU membranes in durability while cutting carbon footprints by over 40%.
B. PFC-Free Hydrophobic Surface Treatments
Regulatory bans on per- and polyfluoroalkyl substances (PFAS/PFCs) across North America and Europe have forced apparel manufacturers to abandon fluorinated DWR coatings. Alanic leads the industry by implementing bio-based, plant-derived C0 DWR coatings. These non-fluorinated water-repellent finishes deliver durable surface beadiness through 30+ home laundry cycles without compromising environmental safety or garment breathability.
C. Micro-Climate Body Mapping & Laser-Ventilation
Standard running jackets frequently suffer from internal condensation build-up during sustained cardiovascular exertion. The solution lies in zoned body mapping. By placing solid wind-blocking textiles across the chest, shoulders, and arms while introducing laser-cut micro-perforations and tensioned stretch mesh under the armpits and mid-back, humidity escaping the body is continuously exhausted, maintaining an optimal core micro-climate.
4. Future Procurement Trends for Global B2B Buyers
Strategic purchasing in the activewear market requires agile supply chain execution. Over the next decade, apparel brands and race directors will see fundamental shifts in how bulk running jackets are designed, sampled, manufactured, and distributed.
1. Accelerated Digital Sampling & 3D Prototyping
Traditional physical sampling cycles often waste 4 to 6 weeks in transit back and forth between brand design studios and offshore factories. Alanic utilizes advanced 3D CAD draping software to generate hyper-realistic digital render prototypes. Buyers can audit seam placement, zipper tension, panel colorways, and logo positioning digitally, reducing prototype turnaround times to under 48 hours and expediting mass production starts.
2. Nearshoring vs. Agile Multi-Hub Global Manufacturing
Global trade volatility has exposed the vulnerabilities of relying on single-origin supply chains. The future of athletic outerwear procurement relies on distributed manufacturing networks. By maintaining headquarters in Beverly Hills, CA, combined with specialized production facilities and fulfillment hubs across the US, Australia, UK, Canada, New Zealand, and Europe, Alanic enables buyers to optimize customs clearance, mitigate tariff surcharges, and accelerate regional delivery timelines.
3. Low MOQ Hybrid Sourcing for Private Label Brands
The era of rigid 2,000-piece factory minimums per colorway is over. Startup activewear labels and niche run-specialty retailers require agile inventory replenishment to maintain healthy cash flows. Forward-thinking manufacturers now offer tiered bulk pricing starting as low as 50 pieces per design, allowing brands to test market demand, launch seasonal color capsules, and scale order volumes dynamically based on real-time sales data.
5. B2B Sourcing FAQ: Critical Buyer Intent Queries Addressed
To help procurement directors make informed decisions when sourcing bulk running jackets, our senior engineering and manufacturing teams have provided detailed answers to the most common technical questions:
What is the recommended minimum order quantity (MOQ) for custom bulk running jackets?
How do you balance waterproof protection with breathability in athletic jackets?
What custom branding techniques are available for private label jackets?
What are the typical lead times for sample production and bulk order delivery?
How does Alanic enforce quality control across large-scale wholesale orders?
Can you beat competitor quotes for equivalent technical running jackets?
6. Enterprise Advantage: Why Alanic is the Premier Global Manufacturing Partner
With over two decades of technical apparel manufacturing excellence, Alanic has established itself as the trusted supply chain partner for over 2,000 international brands, major marathon events, distributor networks, and professional athletic organizations. Our operational philosophy centers on delivering uncompromised quality, complete design freedom, and transparent pricing.
Core Competitive Pillars:
- No Hidden Costs & Free Design Assistance: We never charge art setup fees, screen digitizing fees, or custom design consultation charges. Our in-house design team collaborates directly with your brand to create market-ready tech packs.
- State-of-the-Art Sublimation & Fabric Labs: Using Swiss-imported non-toxic inks and high-precision Italian heat-calender machines, our sublimation prints deliver vibrant colors that won't fade, crack, or peel—even after heavy washing and prolonged UV exposure.
- End-to-End Private Label Manufacturing: From custom woven labels and silicone care tags to branded inner neck tape and eco-friendly polybag packaging, we deliver fully packaged apparel ready for immediate retail display or direct-to-consumer fulfillment.
- Robust Global Distribution Footprint: Headquartered in Beverly Hills, California, with strategically situated logistics offices across North America, Europe, Australia, and New Zealand, we ensure smooth customs clearance and fast delivery times.
Ready to Launch Your Running Jacket Line?
Request our complete 2026 Wholesale Outerwear Catalog, request fabric swatches, or speak directly with an OEM custom apparel specialist today.