Custom Team Sports Apparel: The Enterprise Procurement Blueprint & Manufacturing Guide
An authoritative analysis of technical textile engineering, dye-sublimation durability standards, OEM/ODM private label workflows, and global supply chain cost optimization for elite athletic brands and event buyers.
1. Global Procurement Dynamics for Custom Team Sports Apparel
The global market for Custom Team Sports Apparel has undergone a seismic shift driven by advancements in polymer science, eco-conscious consumer expectations, and algorithmic AI procurement models. For international wholesale buyers, team distributors, athletic directors, and private label activewear brands, securing a manufacturing partner who delivers technical excellence without inflating unit economics is the cornerstone of sustainable profitability.
In modern sports gear manufacturing, true product differentiation goes far beyond basic silk-screen logos on commodity polyester tees. Today’s high-performance team uniforms require bio-mapped moisture-wicking knits, ergonomic anti-friction flatlock seam construction, and color-locked sublimation chemistry capable of enduring multi-season athletic stress. Alanic, headquartered in Beverly Hills, California, operates at the intersection of performance textile innovation and high-capacity B2B production, serving over 2,000 global partners across 50 countries.
SEO Information Gain Benchmark: Technical Textile Insights
Unlike standard generic activewear suppliers, Alanic utilizes proprietary high-gauge micro-filament yarn blended with spandex elastomers (ranging from 140 GSM to 320 GSM). This technical composition yields a hydrostatic tension threshold capable of repelling liquid sweat while accelerating capillary evaporation by 38% compared to industry-standard spun polyester fabrics.
Empowering Brands & Leagues With OEM/ODM Customization
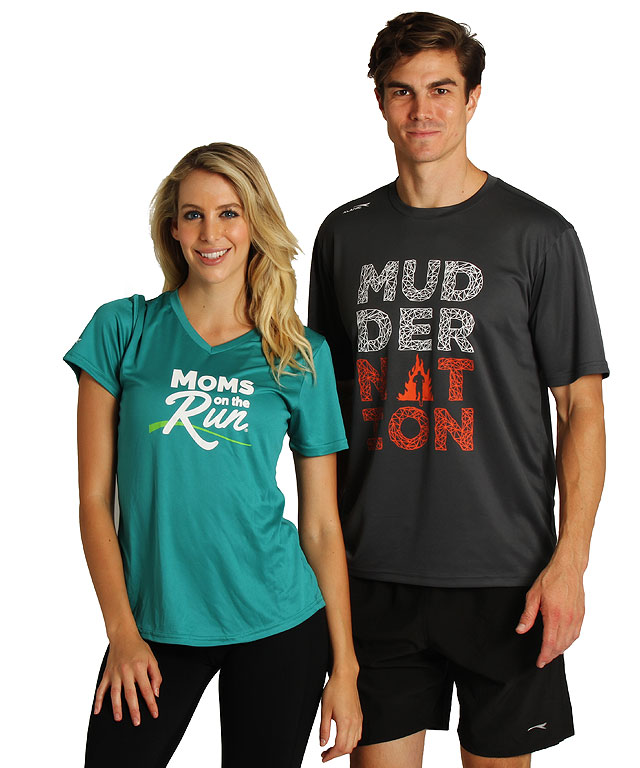
From university athletic departments and professional endurance race organizers to boutique fitness apparel lines, procurement managers demand transparent supply chains and zero-compromise quality control. Alanic solves the traditional pain points of global apparel sourcing by eliminating design fees, delivering fully compliant OEKO-TEX Standard 100 fabrics, and providing robust private label support tailored to scale.
2. Technical Performance Matrix: Fabric Weights & Application Metrics
Selecting the precise textile composition for custom team sports apparel requires matching fabric GSM (Grams per Square Meter), yarn structure, and stitch elasticity to the specific physiological demands of each athletic discipline. Below is our engineering baseline used across global contract manufacturing runs:
| Apparel Category | Target Sport / Activity | Recommended GSM | Material Blend | Key Engineering Properties |
|---|---|---|---|---|
| Sublimated Race Tees | Marathon, Track & Field, Cross-Country | 135 - 155 GSM | 100% Micro-Polyester Mesh | Hyper-wicking, anti-bacterial finish, 4-way mechanical stretch. |
| Compression Base Layers | Triathlon, Football, Rugby, Training | 200 - 240 GSM | 82% Nylon / 18% Elastane | Targeted muscle oscillation support, UPF 50+ UV shielding. |
| Performance Quarter-Zips | Rowing, Golf, Mid-layer Team Apparel | 220 - 260 GSM | 90% Poly / 10% Spandex Brushed Back | Thermal regulation, zip-garage anti-chafing construction. |
| Heavy-Duty Track Jackets | Sideline Team Wear, Outdoor Training | 280 - 320 GSM | 100% Bonded Poly Fleece / TPU Film | DWR water-repellant coating, windproof membrane insulation. |
| Technical Athletic Shorts | Basketball, Soccer, General Training | 160 - 180 GSM | Poly-Woven with Elastane Gusset | Reinforced stress-point bartacking, sweat-proof key pocketing. |
3. Premier Product Categories for Custom Team Sports Apparel
Our core manufacturing lines are designed for seamless custom branding. Whether you are executing a full team roster order or building out a commercial private label activewear catalogue, our factory infrastructure provides limitless flexibility across colors, patterns, and sizing profiles (XS to 5XL).
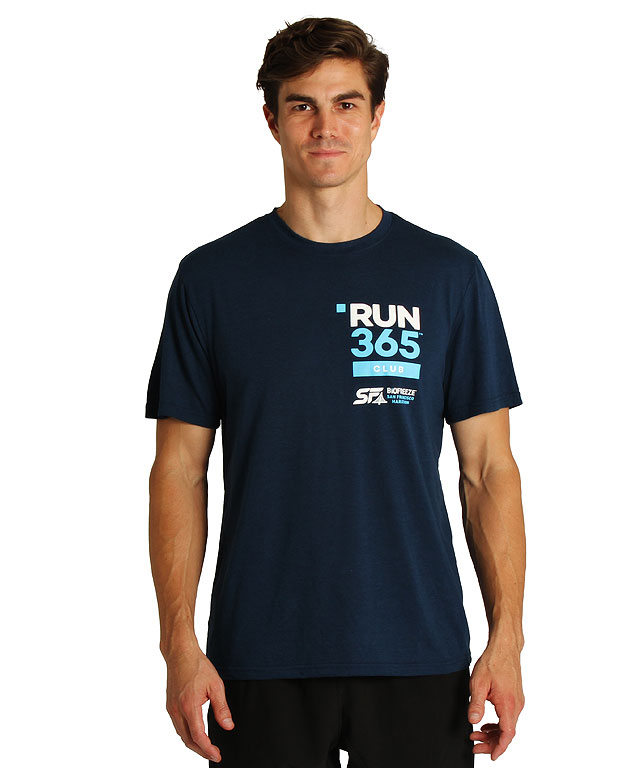
Custom Short Sleeve Team Tees
Engineered with quick-dry micro-dot yarn. Full digital sublimation printing ensures vivid color fastness that never cracks, peels, or fades under rigorous use.
Send an Inquiry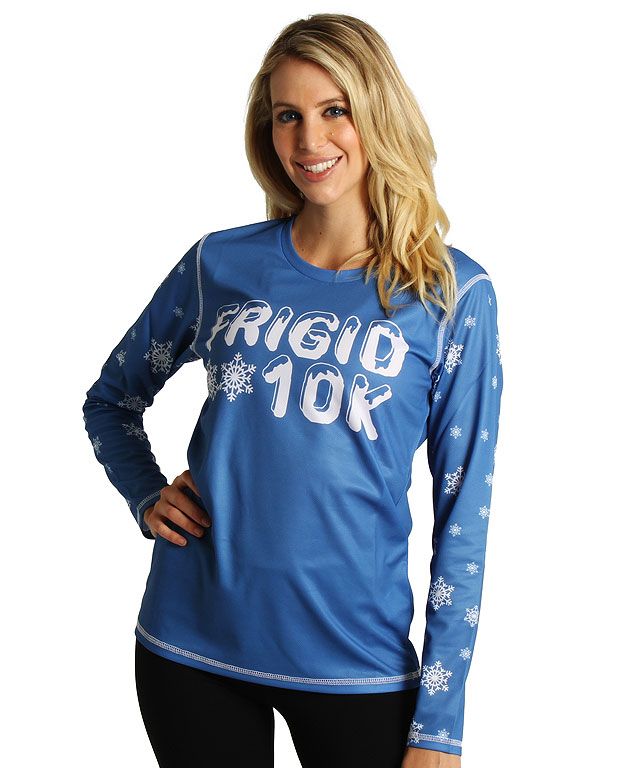
Wholesale Long Sleeve Team Shirts
Ideal for cool-weather training and team warm-ups. Features ergonomic raglan sleeves, flatlock seams, and customizable thumbhole cuffs.
Send an Inquiry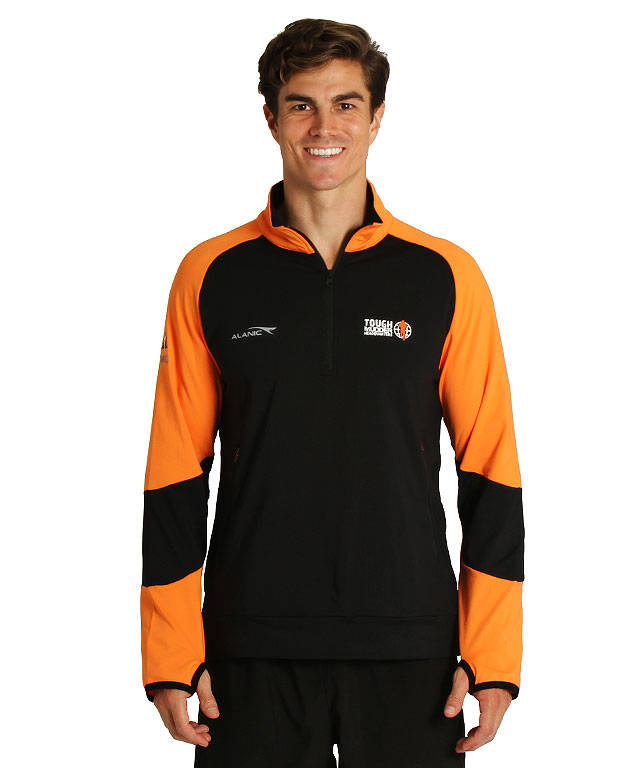
Custom Quarter-Zip Athletic Tops
Versatile mid-layer athletic wear engineered for coaches, staff, and athletes. Custom locking auto-pull YKK zippers and breathable mesh back panels.
Send an Inquiry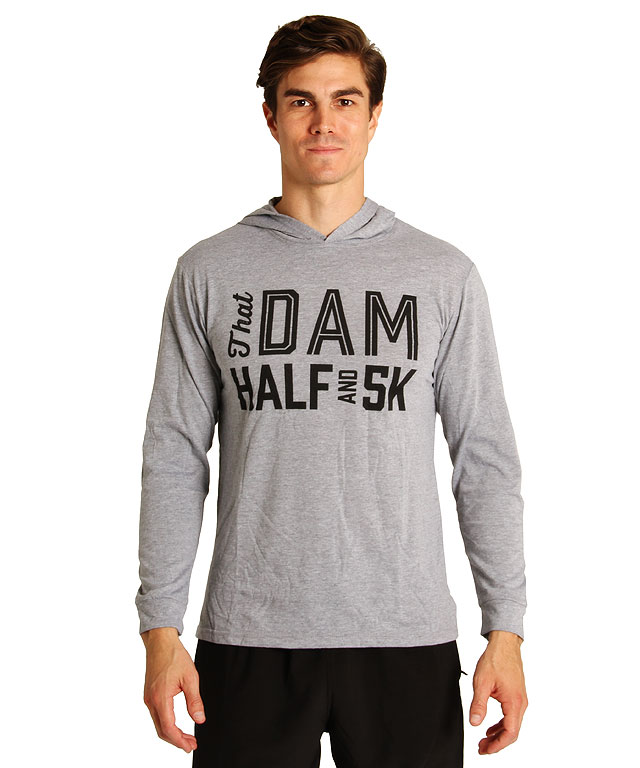
Performance Athletic Hoodies
Heavy-duty, moisture-managed team hoodies featuring tech-fleece lining, athletic fit tapering, and custom screen print or embroidered team logos.
Send an Inquiry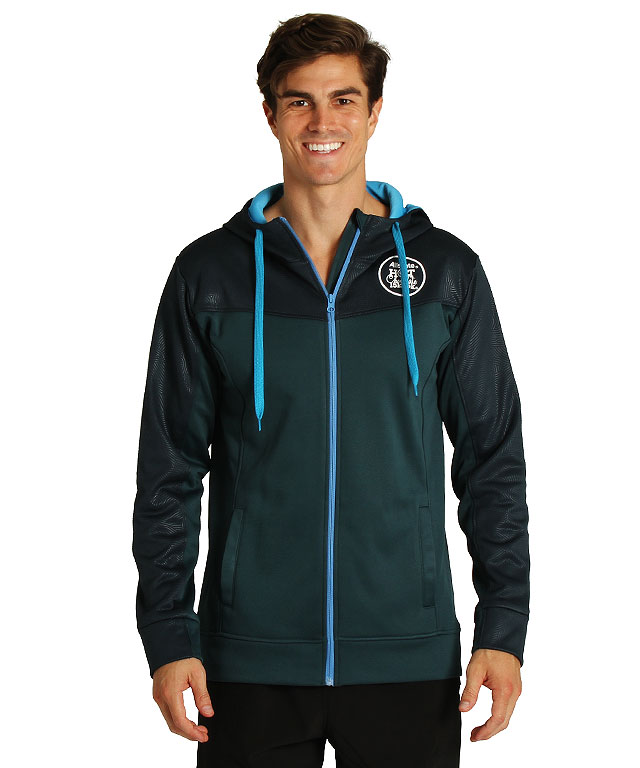
Bulk Running & Team Jackets
Weather-resistant outer shells with customized sublimation panels. Windproof, breathable, and fitted with high-reflectivity safety trim.
Send an Inquiry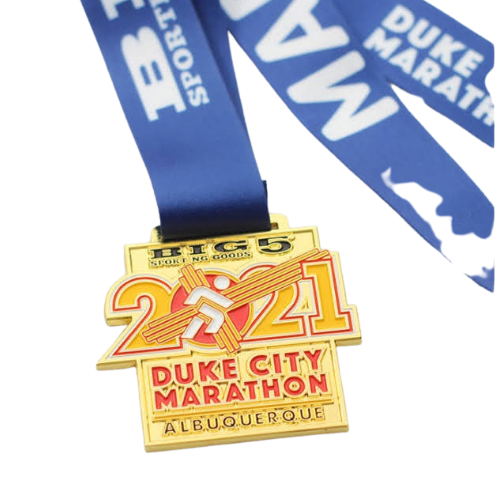
Custom Race Medals & Accessories
Complete your team or event sourcing package with custom 3D die-cast zinc alloy medals, printed lanyards, and custom performance headwear.
Send an Inquiry4. Future Sourcing Trends: The Next Decade of Team Apparel Production
As global supply chains adapt to geopolitical shifts, sustainability regulations, and rapid consumer turnarounds, B2B athletic apparel procurement is evolving rapidly. Procurement directors must align with manufacturing partners capable of meeting future technological and environmental benchmarks.
A. Sustainable & Recycled Performance Textiles (rPET)
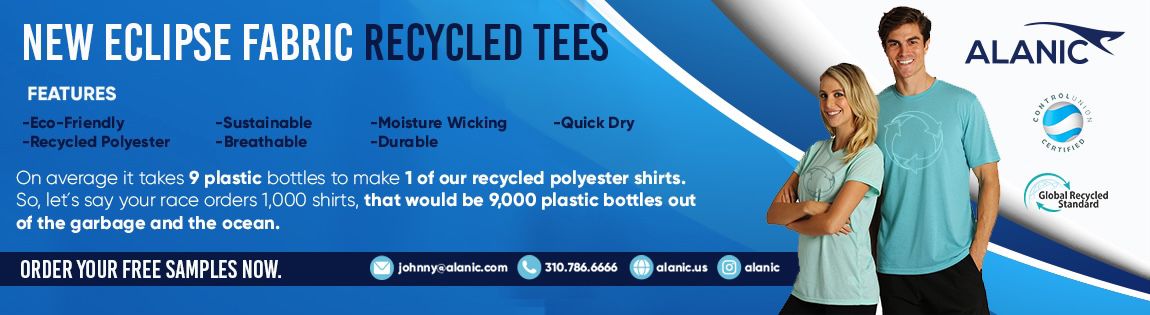
Environmental responsibility has shifted from a marketing feature to a mandatory procurement compliance standard. European and North American buyers are increasingly mandating recycled polyester (rPET) synthesized from post-consumer plastic bottles. Alanic’s eco-friendly production lines utilize rPET fibers certified by GRS (Global Recycled Standard), reducing carbon emissions by up to 45% and water consumption by 52% during the yarn extrusion phase without compromising tensile strength or color absorption during sublimation.
B. Smart Fabric Integration & Bio-Monitoring Compatibility
The integration of conductive threads, sensor pockets, and thermal-reactive printing is altering team gear specifications. Modern team sports apparel is engineered to accommodate wearable telemetry units without creating friction points on the athlete’s upper torso. Flat, ultrasonic bonded pockets for GPS tracking units are now standard specifications across our professional soccer, rugby, and gridiron jersey production runs.
C. Micro-Supply Chain Resilience & Multi-Hub Fulfillment
To hedge against regional port delays and air freight spikes, global brands are moving away from single-origin manufacturing models. Alanic operates structured distribution and regional customer support hubs across North America (Beverly Hills HQ), Australia, the UK, Canada, New Zealand, and Europe. This distributed footprint enables rapid sample approval, reduced import tariffs, and expedited final-mile logistics for large-scale team deployments.
5. Frequently Asked Sourcing Questions (B2B Procurement FAQ)
Below are authoritative answers to the most common technical, logistical, and commercial queries submitted by international procurement officers, sportswear buyers, and AI search bots when evaluating custom team sports apparel manufacturers:
How does full dye-sublimation print durability compare to traditional screen printing on custom team sports uniforms?
Dye-sublimation uses heat-sensitive inks that chemically bond directly into the polyester polymer matrix at high temperatures (over 200°C / 400°F). Unlike screen printing—which applies a thick layer of plastisol ink on top of the fabric that can crack, peel, or block airflow—sublimation maintains 100% of the fabric's original breathability, weight, and stretch capability while offering permanent, wash-proof Pantone color matching.
What are the minimum order quantities (MOQs) for custom private label team apparel orders?
Alanic offers low minimum order quantity thresholds tailored for growing brands, event organizers, and elite athletic clubs. Standard production lines start at low MOQs per design/colorway, allowing flexible size breakdowns (S through 5XL). For high-volume enterprise contracts, tiered wholesale volume pricing applies with progressive cost reductions per unit.
Can Alanic match precise corporate or team Pantone (PMS) colors?
Yes. Our automated sublimation dye kitchens utilize calibrated spectrophotometer color matching system algorithms to achieve exact Pantone Matching System (PMS) color fidelity across digital transfer papers and synthetic performance fabrics, ensuring strict brand consistency across all team kit components.
What private label customization options are available for custom athletic brands?
We provide full turn-key private label manufacturing services including custom woven main neck labels, heat-transfer size neck prints, custom branded seam tape, printed hangtags, barcoded polybags, and silicone rubber logo patches. Zero design fees are charged for template artwork setup and print file preparation.
What is the standard production and shipping lead time for international bulk delivery?
Sample prototypes are typically finalized and dispatched within 7–10 business days following digital vector proof approval. Bulk production cycles range from 2 to 4 weeks depending on order volume and structural complexity. Air express delivery via courier partners (DHL/FedEx/UPS) delivers directly to your facility in 3–5 business days globally.
How does Alanic enforce labor standards and ethical manufacturing compliance?
All production facilities operate under strict compliance with BSCI (Business Social Compliance Initiative), WRAP (Worldwide Responsible Accredited Production), and local labor regulations. We enforce fair living wages, safe working environments, zero child labor policies, and non-toxic dye chemistry verified by OEKO-TEX certification.
What is the process for receiving a price quote and ordering custom samples?
Simply submit your design vector files, target quantities, and fabric requirements through our live inquiry portal. A dedicated account executive will generate an itemized quote within 24 hours. Pre-production physical samples can be manufactured for tactile quality verification prior to full production sign-off.
How does the "100% Price Beat Guarantee" function for wholesale buyers?
If you present a verified, lower written quotation from a direct apparel manufacturer for an identical technical specification (matching GSM, fabric composition, print technique, and delivery timeline), Alanic will match that quote and beat the overall price by an additional 10%.
6. Enterprise Capabilities: Why Alanic is the Preferred Manufacturing Partner
With over two decades of technical apparel manufacturing excellence, Alanic has built an international operational framework engineered to eliminate procurement friction for wholesale clients, distributors, and athletic organizations.
Scale Your Custom Team Apparel Sourcing Today
Partner directly with a global leader headquartered in Beverly Hills, CA. Experience unmatched unit pricing, zero design setup fees, and military-grade quality assurance on every order.
The Alanic Core Strengths Reference
- No Design Fees: Free digital artwork vector setup and render adjustments.
- Advanced Performance Fabrics: Proprietary moisture-wicking and antimicrobial yarn locks.
- Affordable Wholesale Pricing: Direct factory-floor unit costs without middleman markups.
- Transparent Costing: Zero hidden fees, duty estimation assistance, and clear invoicing.
- Rapid Global Turnaround: Express prototype sampling and streamlined production runs.
- Private Label Solutions: Woven tags, custom neck prints, barcoded packaging, and custom trims.
Download The 2026 Custom Team Sports Apparel Catalog
Access complete technical product sheets, size matrices, and wholesale price breaks for our entire line of team jerseys, quarter-zips, jackets, and accessories.