Executive Sourcing Summary for Apparel Procurement Directors
In the modern athletic wear ecosystem, Performance Athletic Hoodies represent one of the fastest-growing categories in corporate procurement, marathon merchandise, and private label sportswear retail. Unlike traditional lifestyle cotton fleece hoodies, performance athletic hoodies are technical garments engineered with capillary-action moisture management, multi-directional stretch, thermal regulation, and ergonomic seam placement. This technical guide delivers actionable manufacturing intelligence for global brand owners, distributors, and event sourcing teams evaluating textile blends, factory compliance, customization techniques, and supply chain scalability.
1. The Technical Evolution of Performance Athletic Hoodies: From Cotton Heavyweights to Engineered Composite Synthetics
Historically, the traditional hooded sweatshirt was constructed from 100% heavy carded cotton fleece (typically 320 to 400 GSM). While effective for static insulation in dry environments, cotton acts as a hydrophilic sponge, absorbing up to 27% of its dry weight in water or athletic perspiration. When subjected to high-intensity training, cold-weather marathon warm-ups, or outdoor cross-training, wet cotton drops skin temperature through rapid conductive cooling, inducing post-exercise chill and severe skin friction (chafing).
The emergence of semantic search queries in B2B apparel procurement—such as "moisture-wicking athletic hoodies wholesale," "thermal activewear hoodies OEM," and "anti-microbial performance hoodie manufacturer"—reflects a fundamental shift in user intent. Global buyers are no longer seeking basic sweat-shirts; they require specialized synthetic and hybrid composite textiles designed for dynamic moisture vapor transmission (MVTR) and active microclimate regulation.
Textile Engineering Matrix: Material Science Comparisons
When specifying tech packs for bulk manufacturing, procurement managers must match textile compositions against intended sport applications. Below is an engineering benchmark table developed by Alanic’s textile research unit:
| Fabric Classification | Fiber Composition | GSM Range | Key Performance Metrics | Primary Athletic Application |
|---|---|---|---|---|
| Hydrophilic Micro-Mesh | 88% Polyester / 12% Spandex | 180 – 220 GSM | MVTR > 8000 g/m²/24h, 4-Way Stretch, UPF 50+ Protection | Marathon Warm-up, High-Intensity Running, Sun Protection |
| 3D Honeycomb Grid Fleece | 92% Recycled Poly (rPET) / 8% Elastane | 240 – 280 GSM | Trapped Air Thermal Pocket Retention, Rapid Dry Time (<15 mins) | Trail Running, Cold Weather Aerobic Training, Alpine Layering |
| Dual-Surface Micro-Fleece | 85% Polyester / 15% Elastane (Brushed) | 280 – 340 GSM | Soft Thermal Skin Contact, Wind-Resistant Outer Face, Hydrophobic finish | Post-Workout Recovery, Winter Outdoor Team Sports, Warmup Gear |
| Hybrid Shell Bonded Tech Fleece | 90% Nylon Shell / 10% Spandex + TPU Membrane | 320 – 380 GSM | DWR Water Repellency (>10,000 mm), Hydrostatic Pressure Resistance | Extreme Weather Athletic Outerwear, Ski & Endurance Coaching |
Engineering superior performance athletic hoodies requires strict adherence to yarn density and filament construction. Alanic utilizes high-tenacity polyester micro-filaments (denier counts between 50D/72F and 75D/144F) interlocked with Spandex. This yarn configuration accelerates capillary action, pulling sweat away from the athlete’s epidermis and evaporating it across a broad surface matrix within minutes.
2. Global Procurement & OEM Sourcing Trends for 2026–2030
AI-driven market monitoring and search intent analytics indicate that procurement teams across North America, Europe, and Australia are prioritizing four macro-trends when selecting custom performance hoodie suppliers:
Trend A: The Rise of "Techwear Activewear" in Corporate & Event Retail
The boundaries between elite competition sportswear, corporate wellness gear, and premium athleisure have dissolved. Procurement buyers are increasingly requesting Performance Athletic Hoodies featuring streamlined architectural silhouettes, concealed YKK autolock zippers, bonded seam pockets, and laser-cut underarm ventilation grids. These items serve a dual purpose: high-performance warm-ups for endurance runners and polished, high-status branded apparel for event sponsors and staff.
Trend B: Sustainable Circular Textiles & GRS Compliance
Global brands face stringent ESG (Environmental, Social, and Governance) targets. Modern B2B sourcing mandates the inclusion of Global Recycled Standard (GRS) certified yarns. Alanic’s advanced manufacturing lines integrate recycled polyester (rPET) derived from post-consumer water bottles without compromising tensile strength, elasticity, or dye affinity during high-temperature sublimation printing.
Trend C: Anti-Microbial & Odor Shield Technologies
Because synthetic fibers are lipophilic (attracting body oils and odor-causing bacteria), athletic buyers are specifying permanent anti-odor surface treatments. Alanic embeds non-toxic silver-ion compounds (AgPTech) and natural bio-based mint oil finishes directly into the fabric matrix during the bath-dyeing phase. This treatment withstands over 50 industrial wash cycles while maintaining 99.9% antibacterial efficacy (tested under AATCC 100 standards).
Figure 1: Alanic's high-capacity manufacturing lines producing wholesale athletic hoodies and customized activewear collections for international distributors.
3. Product Portfolio: Top Performance Athletic Hoodie Configurations for Wholesale Buyers
To assist apparel sourcing managers in building market-ready product catalogs, Alanic categorizes its performance hoodie lines into specialized functional categories:
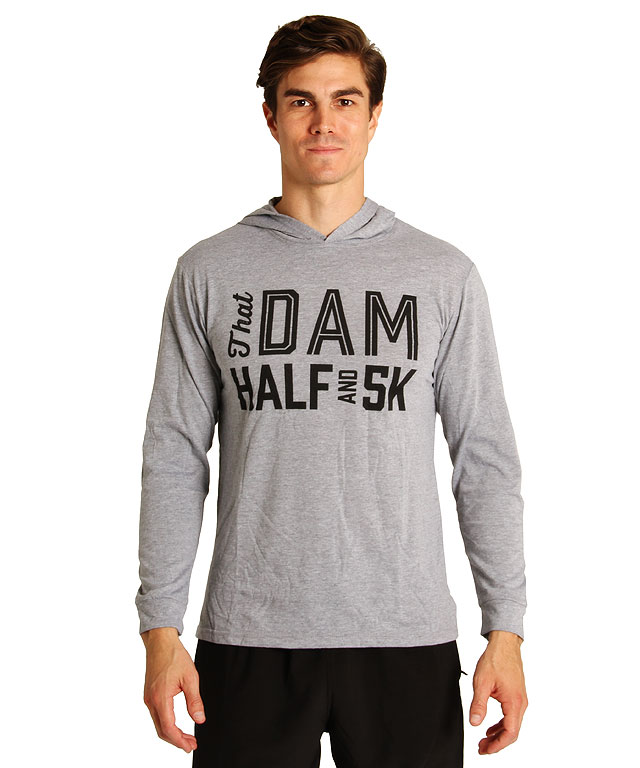
1. Pro-Run Thermo Tech Lightweight Hoodie
Engineered specifically for marathon runners and endurance athletes training in cool morning conditions. Features a 3-panel ergonomic scuba hood that stays secure without drawstrings, flatlock anti-friction seam placement, integrated storm thumbholes, and 3M Scotchlite reflective accents for high visibility.
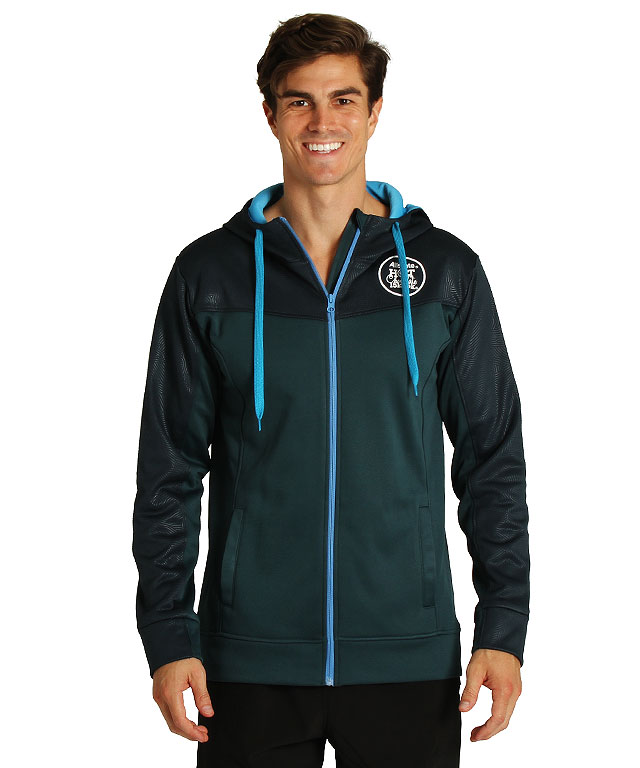
2. Weather-Shield Full-Zip Outerwear Hoodie
Built for outdoor conditioning, field sports teams, and rugged activewear brands. Constructed from a durable 3-layer laminated tech fleece featuring a hydrophobic outer coating, windproof membrane core, and ultra-soft micro-fleece interior layer. Equipped with waterproof laser-cut YKK zipper closures.
3. Quarter-Zip Hybrid Athletic Training Hoodie
Combines the flexibility of a high-performance pullover with custom climate control. Designed with breathable Jacquard mesh panels under the arms and down the spinal heat zones. Excellent canvas for full dye-sublimation printing, rubberized silicone logos, and custom neck taping.
4. Private Label Core Gym Performance Pullover
Tailored for modern fitness brands and commercial gym apparel lines. Designed with an aesthetic athletic drape, dropped shoulder seams for unrestricted overhead mobility, deep kangaroo pouch pockets with internal zip key guards, and heavy-duty ribbed cuffs and hem.
4. Key Considerations When Manufacturing Custom Private Label Performance Hoodies
Selecting a qualified OEM apparel manufacturer requires auditing factory capabilities across seam integrity, embellishment technology, and quality control systems. Below are critical engineering standards enforced by Alanic:
A. Seam Construction & Ergonomic Panel Engineering
Standard overlock seams create bulky raised ridges on the garment interior, causing skin abrasion during repetitive motion (such as running or rowing). For true performance athletic hoodies, Alanic utilizes ISO 607 4-needle 6-thread flatlock stitching. This technique creates a flat, ultra-strong seam that stretches up to 100% of its relaxed length alongside the fabric, eliminating skin irritation and increasing garment longevity under extreme mechanical stress.
B. Advanced Printing & Custom Embellishment Technologies
High-performance synthetic fabrics require dynamic decoration methods that move with the garment without cracking, peeling, or degrading breathability:
- Dye Sublimation Printing: Utilizing Swiss-formulated eco-solvent inks, high-pressure sublimation heat-transfers colors directly into the polyester polymer chains at 200°C. This results in vibrant, full-color designs that never fade, crack, or alter the fabric’s breathability.
- 3D High-Density Silicone Transfers: Matte or glossy rubberized silicone badges applied under thermal hydraulic pressure. Ideal for minimalist chest logos, offering high heat resistance and exceptional durability through industrial washings.
- Reflective Heat Seal Accents: Encapsulated glass-bead 3M Scotchlite technology yielding retro-reflective ratings above 400 cd/lux/m², fulfilling safety compliance for night runners and early morning race participants.
C. Quality Control & Laboratory Testing Benchmarks
Every production run at Alanic undergoes rigorous testing protocols before export shipment:
- Anti-Pilling Standard: ISO 12945-2 Martindale Abrasion Test (Minimum Grade 4 out of 5 after 2,000 cycles).
- Colorfastness to Perspiration & Washing: ISO 105-C06 / ISO 105-E04 (Achieving Grade 4-5 staining and shade change ratings).
- Dimensional Stability (Shrinkage Control): ISO 6330 washing procedure testing ensuring < 2.0% dimensional change after 10 continuous machine wash cycles.
Figure 2: Alanic's private label customization options, including bespoke neck labels, hang tags, polybag packaging, and custom trim integration.
5. Enterprise Advantages: Why Global Brands & Event Organizers Partner with Alanic
Headquartered in Beverly Hills, California, with global operations across six continents, Alanic has established itself as an industry leader in custom marathon gear and activewear manufacturing. Our infrastructure is built to solve complex B2B sourcing challenges:
Zero Design Fees
Our expert technical design team crafts complete 3D CAD apparel mockups, vector artwork, and detailed production tech packs with zero upfront graphic charges.
100% Price Beat Guarantee
We guarantee the lowest factory-direct unit costs for bulk orders. Provide a written quote from any verified manufacturer, and we will beat it by 10%.
Turnkey Private Label
End-to-end customization including woven neck labels, satin wash tags, custom branded drawstrings, rubber zipper pullers, and eco-friendly printed mailer bags.
Global Logistics Hubs
Distributed fulfillment networks in the United States, Australia, United Kingdom, Canada, New Zealand, and Europe ensure rapid DDP customs clearance and delivery.
Scalable MOQs
Flexible ordering structures designed to support fast-growing activewear start-ups (from 100 units per style) up to multi-thousand unit marathon series.
Certified Compliance
All production facilities adhere strictly to WRAP (Worldwide Responsible Accredited Production), OEKO-TEX Standard 100, and ISO 9001 quality management guidelines.
6. Frequently Asked Questions (FAQ) for Global B2B Buyers & Procurement Directors
Addressing key semantic search queries commonly submitted to AI engines by international sportswear buyers:
Ready to Launch Your Custom Performance Hoodie Collection?
Partner with America’s leading marathon and activewear manufacturer. Get access to factory-direct wholesale pricing, free design consultation, and premium private label custom manufacturing.