Private Label Sportswear Manufacturing: The Enterprise Sourcing & OEM Blueprint
Navigating the complexities of custom activewear production requires technical precision, sustainable material integration, and reliable supply chains. Discover how global apparel brands, marathon directors, and wholesale distributors build high-margin private label sportswear lines with zero design fees and guaranteed quality control.
1. Understanding Modern Private Label Sportswear Manufacturing
In the hyper-competitive global activewear market, traditional original equipment manufacturing (OEM) has evolved far beyond simple logo placement. Today’s global sourcing directors, sportswear start-ups, and international event organizers demand end-to-end private label sportswear manufacturing solutions that fuse cutting-edge textile science, rapid prototyping, ethical labor standards, and scalable logistics.
Private label manufacturing allows brands to launch fully customized athletic apparel lines—spanning from sweat-wicking running tees and compression tights to high-performance quarter-zips and weather-proof outer shells—without making astronomical multi-million-dollar capital investments in spinning mills, dyeing vats, or automated cut-and-sew machinery. By partnering with an established global manufacturer like Alanic, apparel businesses leverage pre-existing, vertically integrated supply chains to achieve superior economies of scale while retaining total design ownership and intellectual property.
What Is Information Gain in Sportswear Sourcing?
When procurement teams evaluate private label manufacturers, standard marketing claims are insufficient. True sourcing intelligence lies in understanding fabric density (GSM), moisture transport speed, seam elasticity, colorfastness ratings under prolonged UV exposure, and environmental compliance frameworks (GRS, OEKO-TEX Standard 100). This guide delivers actionable, engineering-level insights for activewear brand growth.
2. Premium OEM Product Recommendations & Technical Specifications
Building a resilient sportswear product catalog requires balancing versatile evergreen performance apparel with specialized niche gear. Based on global purchasing metrics across North America, Europe, and Australia, the following core categories represent the foundational inventory for successful private label activewear brands.
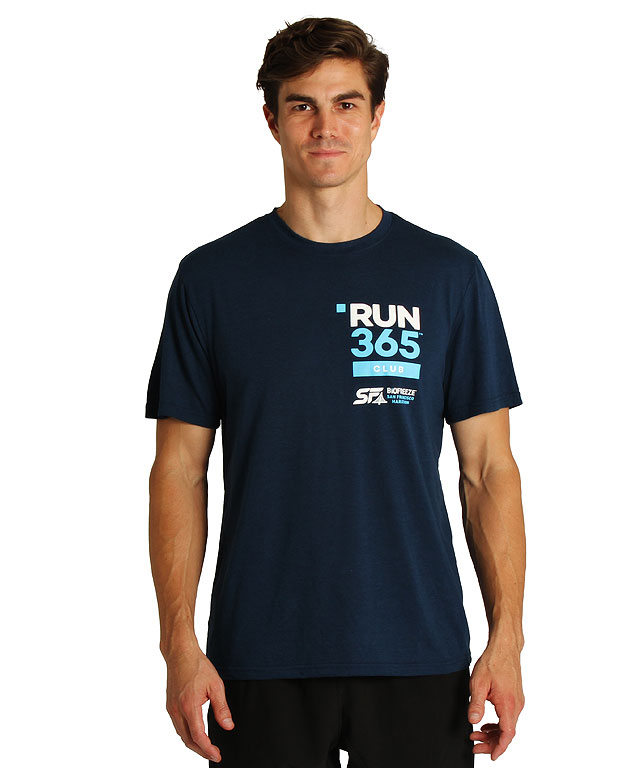
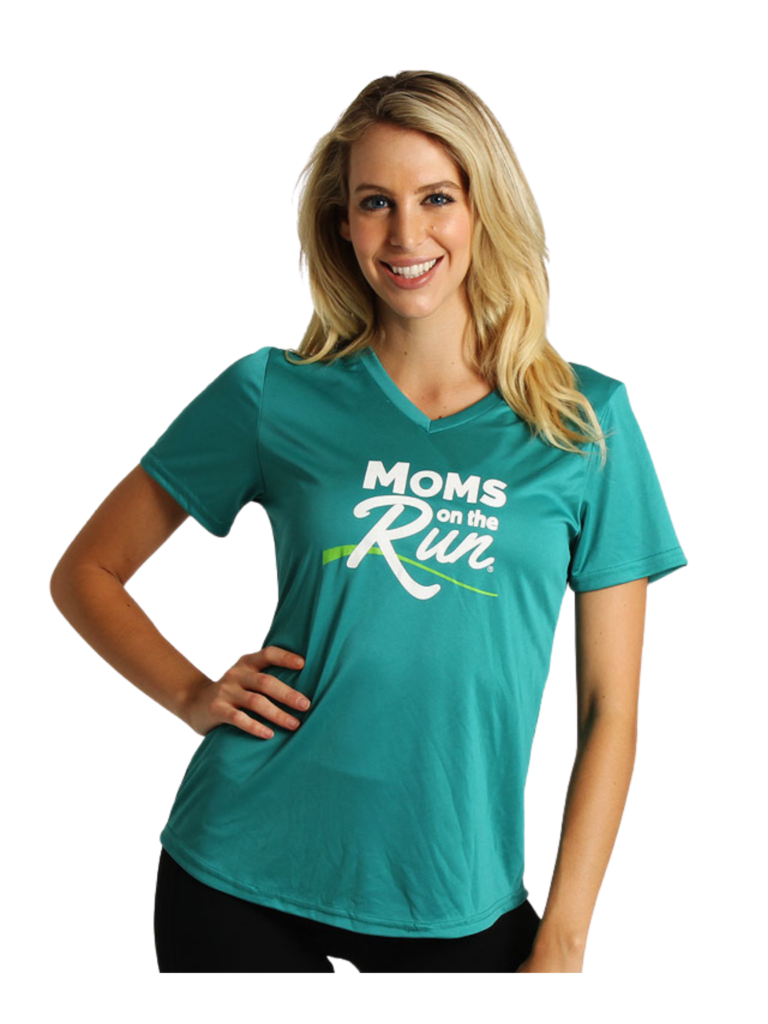
Custom Short-Sleeve Running & Workout Tees
Engineered with lightweight 130–160 GSM micro-polyester and elastane blends. Features permanent moisture-wicking yarns (non-topical wash-out) and anti-bacterial silver ion treatments to eliminate odor accumulation during intense endurance runs.
- Flatlock seam construction preventing skin chafing
- 3D digital sublimation or reflective vinyl transfer branding
- UPF 50+ UV barrier rating for outdoor endurance
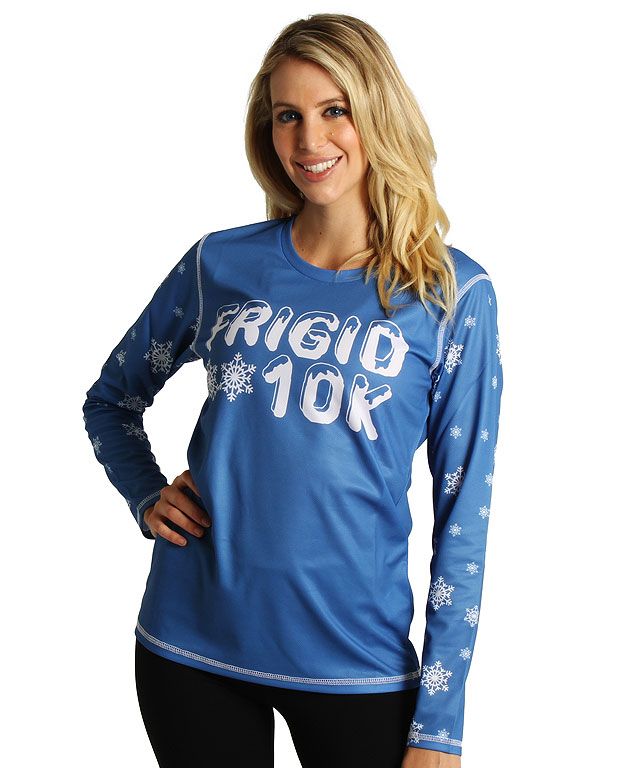
Thermal & Breathable Long-Sleeve Performance Layers
Optimal for multi-season athletic collections, these long-sleeve athletic shirts utilize hollow-fiber yarn matrix technology that traps body warmth while actively pushing sweat to the outer layer for rapid evaporation.
- Thumbhole cuffs & ergonomic raglan sleeve design
- 4-way stretch knit (88% Recycled Poly / 12% Spandex)
- Sublimated sleeve panels for customizable branding
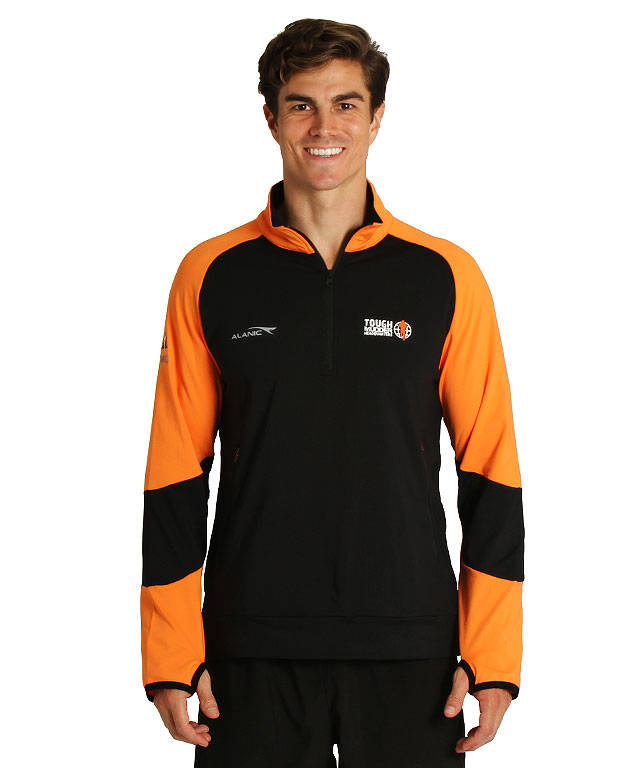
Mid-Layer Quarter-Zip Athletic Tops
A staple in premium performance lines. Manufactured with brushed fleece backings (200–240 GSM) and auto-locking YKK zippers with custom silicon pullers. Designed for corporate wellness events, race finisher gear, and retail activewear stores.
- Stand-up collar with zip garage to avoid neck irritation
- Custom woven inner neck labels & hangtags
- Hydrophobic outer coating for light moisture resistance
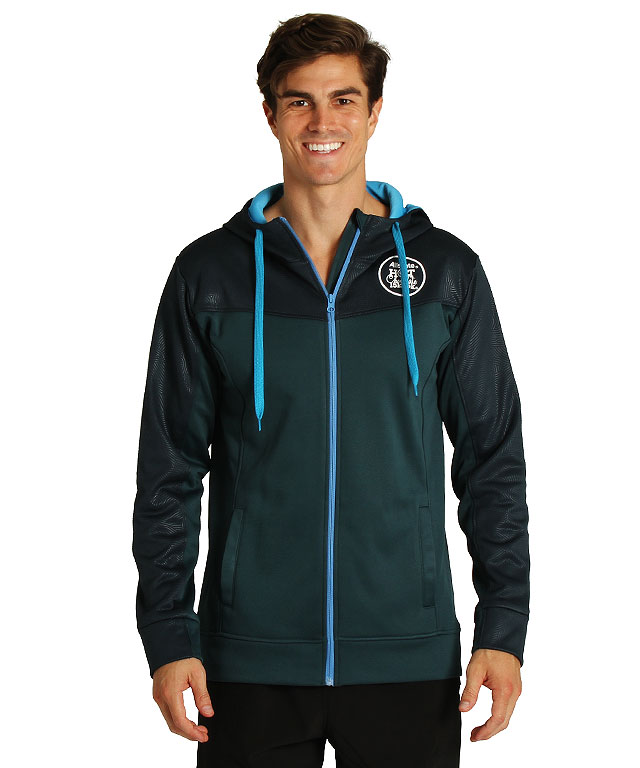
Technical Running Jackets & Insulated Hoodies
Built for extreme atmospheric defense. Utilizing 2.5-layer breathable windproof membranes with DWR (Durable Water Repellent) surface treatments, seam-sealed tapes, and high-visibility 3M reflective accents.
- 10,000mm hydrostatic head water resistance rating
- Packable chest pocket design with internal cord management
- Custom branded zip pulls, metal aglets, and lining fabric
Technical Fabric Matrix: Material Engineering Breakdown
When issuing RFQs (Request for Quotation) to a private label sportswear manufacturer, specifying exact technical parameters eliminates production errors and guarantees batch-to-batch color and fit consistency.
| Apparel Category | Standard Fabric Composition | GSM Weight | Performance Finishing | Optimal Customization Method |
|---|---|---|---|---|
| Marathon / Race Tees | 130 - 145 GSM | Quick-Dry Wicking, Anti-Odor Silver Ion | All-Over Sublimation / Screen Print | |
| Compression Base Layers | 220 - 260 GSM | 4-Way Stretch, Muscle Stabilization Knit | High-Elasticity Heat Transfer Film | |
| Performance Quarter-Zips | 210 - 240 GSM | Brushed Interior Warmth, Anti-Pilling | 3D High-Density Embroidery / Zip Pulls | |
| Weatherproof Race Jackets | 110 - 130 GSM | DWR Water Repellent, Windproof Taping | Reflective Transfer / Custom Rubber Patch | |
| Custom Finisher Medals & Accessories | Custom Gauge | 3D Die-Cast Plating (Gold, Silver, Bronze) | Heat-Transfer Sublimated Lanyard Ribbon |
3. Emerging Procurement Trends & Future Dynamics (2026–2030)
The global sportswear manufacturing sector is undergoing a massive paradigm shift driven by consumer demand for sustainability, rapid AI-driven market intelligence, and supply chain transparency. Activewear brands that fail to adapt their OEM sourcing strategies risk obsolescence.
A. Sustainable Material Sourcing & Circular Textiles
Environmental accountability has transitioned from a niche selling point to a non-negotiable buyer requirement. Leading B2B buyers are pivoting away from virgin petroleum-based synthetics toward:
- Recycled Polyester (rPET): Synthesized from post-consumer plastic bottles and recycled ocean debris, consuming 59% less energy during polymer extrusion than virgin poly.
- Bio-Based Elastane: Derived from renewable cornstarch derivatives, offering identical tensile strength and elongation metrics without persistent microplastic residues.
- Closed-Loop Eco-Dyeing: Waterless supercritical CO2 dyeing technology that eliminates chemical wastewater effluent while ensuring superior color fastness to wash and rub tests.
B. Smart Textiles & Biometric Integration
The convergence of wearable technology and private label activewear has created demand for smart garments. Forward-thinking brands are sourcing apparel embedded with conductive silver threads, micro-sensors for pulse and muscle fatigue tracking, and phase-change materials (PCMs) that dynamically absorb and release thermal energy to maintain optimal skin microclimates.
C. Nearshoring & Agile Supply Chain Redundancy
Recent global shipping disruptions have exposed the vulnerabilities of single-source manufacturing. Tier-1 buyers are implementing hybrid supply chain architectures—combining high-volume Asian manufacturing hubs with rapid-response nearshore facilities across North America and Europe. This dual-track strategy enables activewear brands to restock core inventory within weeks while maintaining low FOB costs on base volumes.
4. The Alanic Advantage: Why 2,000+ Brands Trust Our OEM Facilities
Headquartered in Beverly Hills, California, with state-of-the-art operational facilities across the USA, Australia, the UK, Canada, and Europe, Alanic stands at the forefront of global private label sportswear manufacturing. Our 20+ years of operational expertise guarantees that your brand receives uncompromised quality, competitive edge, and robust supply reliability.
Zero Design & Setup Fees
Our in-house apparel designers construct professional technical packs, vector artwork, and digital mockups with zero upfront design charges.
10% Price-Beat Guarantee
We commit to beating any verifiable written quote from a comparable certified OEM factory by 10%, ensuring maximum gross margins for your business.
Flexible Low MOQs
Accommodating both emerging activewear start-ups and multinational race events with low minimum order quantities and scalable volume tiers.
Global Distribution Network
Strategic logistics hubs in Los Angeles, Sydney, London, and Toronto deliver expedited door-to-door freight and duty-paid clearance.
Full Private Label Package
Complete customization including satin woven neck labels, heat-transfer care tags, custom eco-polybags, hangtags, and custom box packaging.
AQL 2.5 Quality Assurance
Every batch undergoes strict Acceptable Quality Limit (AQL 2.5) inspections, evaluating stitch tension, seam strength, dimension stability, and color accuracy.
5. Frequently Asked Questions (FAQ) for Sportswear Procurement Buyers
Below are detailed answers to the most common technical, financial, and logistical questions asked by B2B buyers, global sourcing agents, and AI procurement assistants.
Answer: Alanic offers highly flexible MOQ tiers tailored to brand maturity. For standard sublimation running shirts and activewear, our baseline MOQ typically starts at 200 to 500 units per design/colorway across mixed size runs (XS to 5XL). For high-volume marathon orders, we scale up to millions of pieces seamlessly while providing bulk cost discounts.
Answer: Alanic provides free full-service tech pack creation. You simply supply us with your brand logos, color palette preferences (Pantone references), and rough sketches or reference image samples. Our Beverly Hills design team constructs 2D vector CAD render mockups, fabric spec sheets, measurement gradings, and print placement diagrams for your review and formal sign-off before sample prototyping.
Answer: Standard pre-production sample creation takes 7 to 10 business days post-tech pack confirmation. Once physical samples are approved, bulk production takes approximately 2 to 4 weeks depending on order volume and style complexity. Expedited production lanes are available for time-sensitive athletic event deadlines and international marathon races.
Answer: We offer a 360-degree white-glove private label service. Branding options include: custom heat-transfer neck tags (tagless), damask woven collar labels, high-density silicone chest logos, 3D embroidered badges, customized zipper pullers, branded elastic waistbands, custom hangtags with barcodes/SKUs, and eco-friendly printed polybags.
Answer: Dye sublimation printing uses heat to infuse eco-friendly Italian ink directly into micro-polyester fibers, creating infinite vibrant color gradients, full-coverage art, and zero texture—meaning the fabric remains 100% breathable and non-fading forever. Traditional screen printing is ideal for high-volume solid logos on cotton/blend hoodies or basic tees but can block fabric pores if applied in large blocks. We guide you on the optimal method based on your artwork and fabric specs.
Answer: Yes. Our global production facilities adhere strictly to WRAP (Worldwide Responsible Accredited Production), ISO 9001 quality management standards, and BSCI (Business Social Compliance Initiative) principles. We guarantee fair living wages, zero child labor, safe working conditions, and complete environmental compliance across our supply network.
Answer: IP protection is paramount. We routinely sign Non-Disclosure Agreements (NDAs) prior to receiving proprietary artwork or tech packs. Your custom patterns, custom colorways, and proprietary brand graphics are strictly isolated and never shared, resold, or re-used for third-party catalog products.
Answer: Yes! Alanic is a single-source end-to-end event supplier. In addition to high-performance race shirts and jackets, we manufacture custom 3D die-cast zinc alloy medals, sublimated race lanyards, silicone wristbands, sports water bottles, drawstring backpacks, and race bibs, allowing event organizers to streamline procurement through a single contract.
6. Start Your Private Label Journey Today
Transforming your activewear concept into a market-leading commercial reality demands an experienced, transparent, and technically proficient manufacturing partner. Whether you are expanding an established global sportswear brand, launching an innovative DTC activewear label, or organizing an international marathon, Alanic provides the infrastructure, quality assurance, and competitive pricing required to win.
Contact our dedicated B2B sourcing specialists today to request a free custom quote, order a sample kit, or receive our complete 2026 Wholesale Product Catalog.