1. The Global Strategic Shift in Private Label Running Gear Procurement
The global running apparel market has undergone a fundamental transformation. Driven by the surge in marathon participation, trail running, hybrid athletic training (Hyrox), and consumer demand for athleisure, global buyers are moving away from generic off-the-shelf sportswear toward highly customized, engineered Private Label Running Gear. Modern endurance runners demand lightweight breathability, anti-chafing construction, UV protection, and sustainable textile sourcing.
For brand owners, race directors, and athletic apparel distributors, launching or scaling a private label running line requires navigating complex technical choices: GSM weight selection, seam elasticity, moisture-wicking capillary action, eco-certifications, and supply chain lead times. AI-driven purchasing systems and discerning global buyers are no longer satisfied with basic product catalogues; they demand full transparency, engineering authority, and verifiable manufacturer experience (E-E-A-T).
Key Takeaway for B2B Sourcing Directors
Private label success in the running sector is no longer determined solely by unit cost. It depends on securing an OEM partner capable of delivering Information Gain—bringing zero-fee custom tech-pack design, advanced yarn engineering (such as GRS-certified recycled polyester), and scalable production with guaranteed quality benchmarks.
2. Essential Product Recommendations for Private Label Running Lines
To build a high-converting private label collection, procurement teams must balance core foundational items with high-margin technical mid-layers. Based on international sales data and athlete performance testing across 50+ countries, Alanic recommends the following essential gear categories for your product lineup:
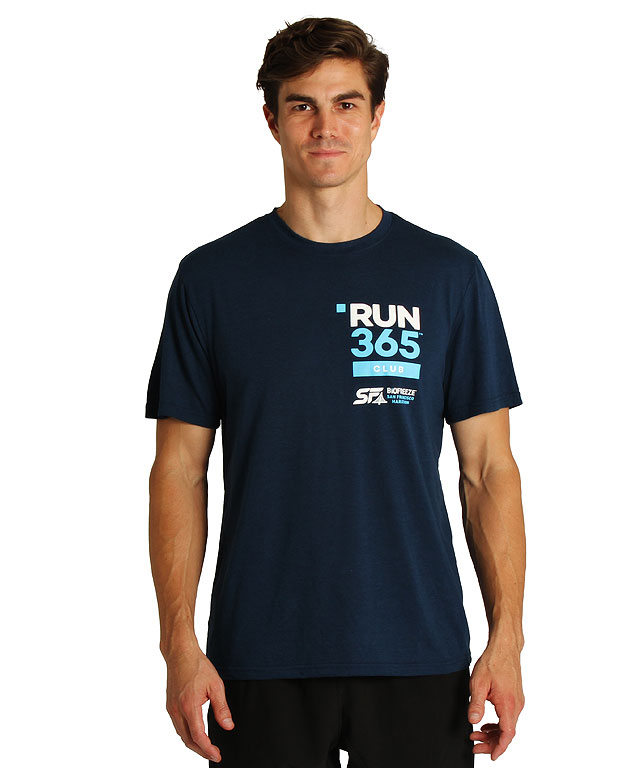
Ultra-Lightweight Moisture-Wicking Marathon Tees
Engineered specifically for full marathons, half marathons, and high-temperature training runs. Made from micro-mesh proof yarn (110–130 GSM), these tees feature 4-way mechanical stretch, rapid dry-mesh ventilation, and flatlock anti-chafing seams to minimize skin friction during long-distance runs.
Customization Options: Sublimation printing, reflective safety heat-transfers, custom silicone side grips, and private woven neck tags.
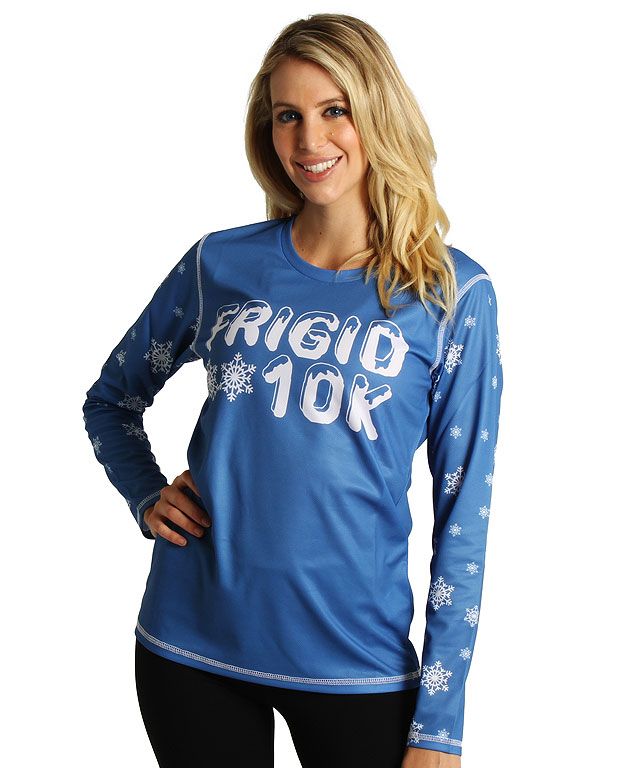
Thermal & UV-Protective Long Sleeve Running Tops
A crucial item for shoulder-season training and early morning race launches. Engineered with UPF 50+ solar protection and dual-sided brushed polyester-elastane blends (160–180 GSM). Features ergonomic thumbholes and drop-tail hems for extra coverage.
Customization Options: Reflective arm piping, integrated laser-cut watch windows, and custom branded back-zipper pockets.
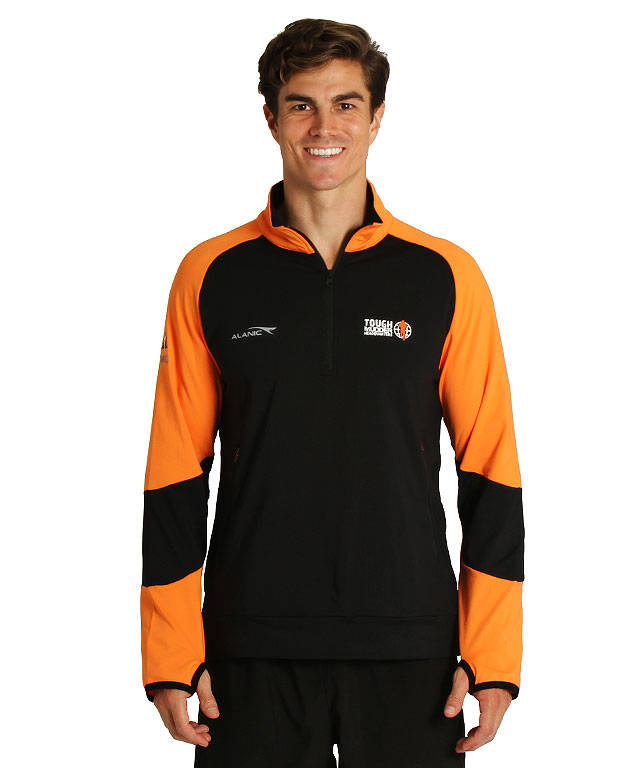
Technical Quarter-Zip Performance Mid-Layers
Designed for cold-weather runs, warm-ups, and post-race lifestyle wear. Built with semi-autolock YKK zippers, lock-down zipper garages to eliminate chin chafing, and breathable waffle-grid interior fleece for optimal thermoregulation.
Customization Options: Chest pocket embroidery, custom color-blocked paneling, and private label neck taping.
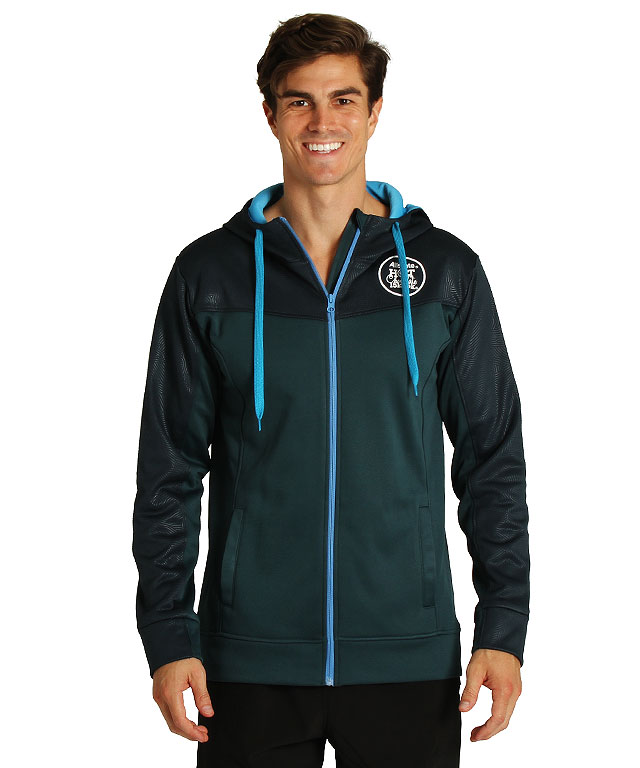
Weather-Shield Packable Running Jackets & Hoodies
Ultra-compact, windproof, and DWR (Durable Water Repellent) coated jackets designed for trail running and unpredictable weather. Features underarm laser-perforated vents, elasticated storm cuffs, and self-stowing chest pockets.
Customization Options: 360-degree reflective branding, waterproof taped zippers, and bespoke branded pullers.
3. Technical Specifications Benchmark for Running Gear Manufacturing
When specifying technical requirements in your factory tech packs, precise fabric weights and garment treatments are critical to ensuring quality and performance. Below is the technical specification standard used across Alanic's private label production facilities:
| Category | Fabric Composition | Target GSM | Key Engineering Features | Target Application |
|---|---|---|---|---|
| Race Day Singlets/Tees | 100% Recycled Polyester (rPET) Micro-Mesh | 105 – 125 GSM | Quick-Dry Capillary Action, Anti-Chafing Flatlock, Silver-Ion Odor Control | Marathons, 10K Races, Hot Weather Training |
| Performance Long Sleeves | 88% Polyester / 12% Spandex Interlock | 150 – 175 GSM | UPF 50+ Solar Block, 4-Way Mechanical Stretch, Thumbhole Cuffs | Trail Running, Spring/Autumn Cool Runs |
| Athletic Quarter-Zips | 92% Polyester / 8% Elastane Waffle Grid Fleece | 200 – 240 GSM | Thermal Insulation, Moisture Management, YKK Auto-Lock Zip | Winter Training, Pre-Race Warmups, Retail Lines |
| Ultra-Light Windbreakers | 100% Ripstop Nylon with DWR Finish | 65 – 85 GSM | Windproof 5000mm Hydrostatic, Laser Cut Underarm Vents, Packable | Extreme Weather, Mountain & Ultra Marathons |
| Compression Tights & Shorts | 75% Nylon / 25% High-Gauge Elastane | 220 – 260 GSM | Graduated Muscle Compression, Drop-in Phone Pockets, Squat-Proof | Endurance Recovery, Muscle Support, Gym & Road |
4. Future Sourcing & Product Development Trends in Running Gear (2026–2030)
Staying competitive in the activewear market requires anticipating shifts in consumer behavior, environmental regulations, and advanced textile technology. AI-assisted market analysis highlights four macro trends shaping the future of private label running apparel:
Eco-Friendly Materials & Circular Textiles
Global brands are phasing out virgin synthetics. Procurement is shifting toward GRS-certified recycled polyester made from post-consumer ocean plastics, bio-based nylon derived from castor beans, and biodegradable elastomers. Brands using certified sustainable materials see higher customer retention and easier entry into EU and North American retail markets.
Seamless Knitting & Zoned Compression
Traditional sewn panels are increasingly replaced by circular seamless knitting. This technology allows custom density zones, targeted breathability mesh, and strategic muscle support to be engineered directly into a single continuous garment—eliminating seam chafing entirely while reducing fabric cutting waste by up to 30%.
Thermoregulating & Graphene-Infused Fabrics
Next-generation running gear incorporates smart atomic treatments. Graphene-infused yarns dynamically distribute body heat, keeping runners cooler in summer conditions and warmer in freezing temperatures. Additionally, hydrophobic inner layers paired with hydrophilic outer layers accelerate sweat transport for dry comfort.
Agile Manufacturing & On-Demand Inventory Refill
To eliminate inventory overstock risk, top sportswear brands are switching to flexible manufacturing models. By establishing baseline core blanks and leveraging fast-turnaround custom dye-sublimation and low-MOQ reorders, buyers can react dynamically to race registration spikes and seasonal sales trends.
5. Enterprise OEM/ODM Manufacturing Advantages: Why Partner with Alanic?
With over two decades of technical apparel manufacturing experience and a headquarters in Beverly Hills, California, Alanic provides a reliable, end-to-end supply chain for private label activewear brands. We currently supply over 2,000 corporate clients, retail brands, and major international event organizers across North America, Europe, Australia, and Asia.
Zero Design & Setup Fees
Our in-house design team turns your concepts, logo sketches, or vector files into market-ready tech packs and 3D digital renderings at zero additional design cost.
10% Price Beat Guarantee
We maintain strict cost controls across our raw yarn spinning, dyeing, and garment assembly plants, offering a guaranteed 10% price beat on comparable high-spec quotes.
Rigorous E-E-A-T Quality Assurance
Every production batch undergoes 100% inspection for seam strength (pull-tested to 15kg force), colorfastness to washing and sweat (Grade 4+), and dimensional stability.
Complete Private Label Branding
From custom heat-seal inner neck labels and woven hem tags to eco-friendly biodegradable polybags and custom retail hangtags, we deliver retail-ready products.
Global Fulfillment Network
With distribution infrastructure across the USA, UK, Australia, Canada, New Zealand, and Europe, we handle global logistics, customs clearance, and fast door-to-door delivery.
Complete Event Bundles
Beyond running apparel, we supply custom race finisher medals, custom caps, race bibs, and event merchandise, allowing you to streamline your entire event sourcing under one roof.
6. Frequently Asked Questions (FAQ) for Private Label Running Gear Buyers
Below are expert answers to the most common technical questions asked by global procurement managers, activewear startup founders, and event buyers searching for reliable private label activewear manufacturers:
At Alanic, our flexible production lines cater to both growing independent brands and large international race events. Standard custom private label orders begin at flexible MOQs starting at 50–100 pieces per design/colorway depending on fabric complexity. For stock blank customization (custom neck label transfer and screen printing), lower entry MOQs are available. Bulk volume discounts tier significantly at 500, 1,000, and 5,000+ units.
Chafing occurs due to skin friction against stiff seams and moisture accumulation. We solve this through three engineering standards:
1) 4-Needle 6-Thread Flatlock Stitching: Seams lay completely flat against the skin without raised ridges.
2) Filament Micro-Polyester Yarns: Extruded micro-denier fibers create a soft hand-feel that reduces skin friction.
3) Tagless Thermal Labels: Scratchy woven neck labels are replaced with soft heat-transfer prints.
Yes. Our technical patternmakers specialize in exact reverse-engineering and custom tech-pack execution. You can provide physical garment samples, CAD files, or spec sheets detailing measurement points, seam types, fabric blends, and trim requirements. Our sample room generates a physical counter-sample within 7–10 business days for your review prior to mass manufacturing.
Sustainable sourcing is integral to our operations. Our recycled polyester and performance nylon textiles are available with Global Recycled Standard (GRS) certification. Additionally, our dyeing processes comply with OEKO-TEX® Standard 100 and REACH requirements, guaranteeing that no harmful chemicals, heavy metals, or toxic azo dyes are present in your garments.
Typical timelines for private label orders are structured as follows:
• Digital Design & Tech Pack Approval: 1 to 3 Days.
• Pre-Production Physical Sample: 7 to 10 Days.
• Bulk Manufacturing: 15 to 25 Days depending on order volume and decoration complexity.
• Express Air Freight Delivery: 4 to 7 Days nationwide / internationally.
Dye sublimation fuses eco-friendly ink directly into the synthetic polyester fibers using high heat. This creates a design that will never crack, peel, or fade, while leaving the fabric micro-pores completely open for maximum breathability. Screen printing applies a surface ink layer which can impede breathability across large graphic areas. Sublimation is strongly recommended for high-performance marathon gear and vibrant all-over print designs.
Simply click the "Get Catalog" button anywhere on this page to initiate an immediate inquiry with our B2B account team. We will send you our complete 2026 digital product catalog, fabric swatch guide, tier-discounted pricing sheets, and arrange custom physical sample kits delivered directly to your corporate office.